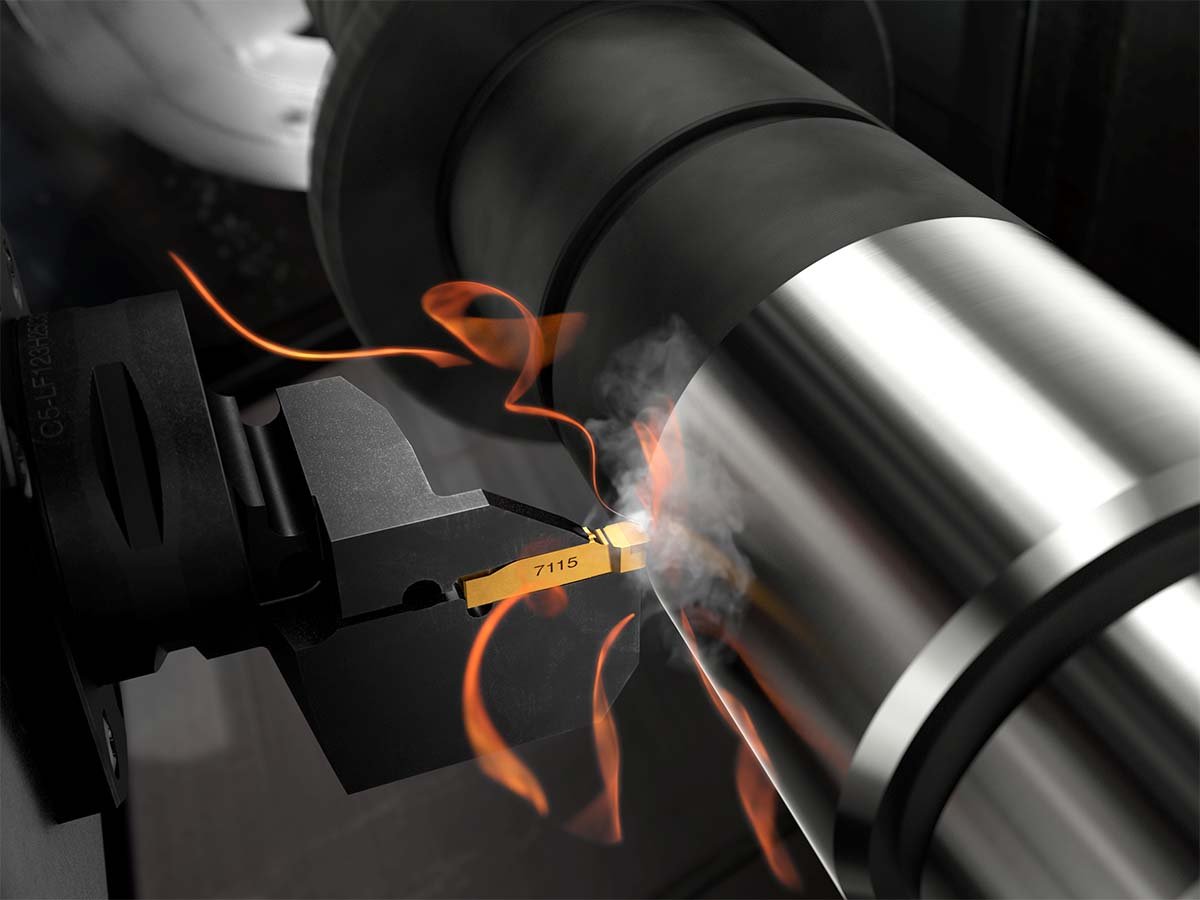
Hard part turning offers manufacturers the opportunity to replace expensive grinding processes, reduce cycle times, and improve machining productivity. However, as with many advanced machining techniques, success depends on overcoming a number of specific challenges. Ralph Löwenau, Product Solution Specialist for Turning at Sandvik Coromant, an expert in metalcutting and production solutions, explores the obstacles manufacturers face in hard part turning and how these can be transformed into opportunities for greater efficiency and profitability.
Hard turning generally refers to the machining of parts with a hardness greater than 45 on the Rockwell hardness scale (HRC). For context, mild steel has a hardness between 10 and 20 HRC, while hardened steel parts used in the automotive and aerospace industries can have a hardness between 45 and 70 HRC.
Turning hard parts is made possible by super-hard cutting tool materials such as cubic boron nitride (CBN) and advanced ceramics. These materials are second only to diamond in hardness, meaning they can withstand the extreme forces and temperatures generated when cutting materials such as hardened steel.
Unlike conventional carbide inserts, which would wear almost instantly under these conditions, CBN grades maintain cutting edge strength and resist both abrasive wear and thermal shock. Additionally, the inserts are designed with special cutting edge preparations and coatings that help manage heat, reduce chipping, and ensure consistent tool life. However, even with the best tools available, turning hard parts still presents challenges.
Exploring common challenges
The extreme hardness of the workpieces can accelerate insert wear, and if tools are not carefully selected or process parameters are not optimized, chipping and edge breakage can occur. Achieving the required surface finish and dimensional tolerances places additional demands on machine setup, toolholder stability, and cutting data.
Hard part turning can be an excellent substitute for grinding, as it can provide comparable quality while reducing cycle times. However, many operators consider grinding the benchmark for surface finish, and achieving comparable quality is important when choosing an alternative method.
High hardness leads to increased cutting forces and significant heat in the cutting zone. This can push the insert temperature above 1000°C, with the risk of thermal cracking, accelerated crater wear, or even workpiece deformation. Without the right insert material and optimized cutting conditions, this additional heat can degrade tool performance and compromise dimensional stability.
Seize the opportunities
To overcome these challenges and succeed in hard part turning, manufacturers should consider tool selection and process planning as strategic investments. CBN grades are the best choice for hard part turning, with many modern grades featuring optimized edge preparations that offer both wear resistance and edge security, allowing for greater stability and increased productivity.
There are two typical preparations for CBN inserts: S-type and T-type. S-type inserts have the best edge line strength and are resistant to microchipping for a more consistent surface quality. T-types are ideal for surface finishes with continuous cuts and minimize burr formation in interrupted cuts.
To further improve part quality, process optimization is equally crucial. Manufacturers should consider their hard turning strategy from the outset, even before the materials are actually hardened. When soft turning, before heat treatment, adding small angled edges to remove sharp edges (known as chamfering) and machining rounded transitions instead of sharp edges (also known as radiusing) can help prevent imperfections that could be transferred to the hardening process, where they would then be more difficult to remove.
When turning hard parts, it's recommended not to jerk the tool out of the cut when entering or exiting. Instead, smooth entry and exit helps prevent stress buildup and edge damage, which can compromise both tool life and component quality.
Hard part turning is a valuable machining strategy when manufacturers seek to improve production efficiency and streamline their processes. However, it is not without its complexities. Choosing the right inserts, machine stability, and careful process planning are all critical to successful turning. Following expert guidance and leveraging advanced tooling solutions can help manufacturers achieve grinding-quality results with shorter cycle times and lower costs.
Sandvik coromant returns to bi-mu 2026 with an entirely digital booth.
Sandvik Coromant, a world leader in metalworking and manufacturing solutions, will return to BI-MU 2026 from October 13 to 16, 2026, at Fiera Milano. The company's participation strengthens its position as a technology partner in the transition to connected, data-driven manufacturing. BI-MU 2026 is an international trade fair dedicated to the machine tool sector, bringing together professionals and decision-makers from across the manufacturing sector. The event serves as a key meeting point for presenting innovations in industrial manufacturing and advanced production technologies. As part of its renewed presence, Sandvik Coromant will be exhibiting in Hall 22, among the machine tool manufacturers, with a completely redesigned booth concept (Stand E10). The company will present a fully digital booth designed as an immersive experience, going beyond the traditional product display to focus on integrated solutions, software, data, and value-added services. The booth was designed as an interactive environment where visitors can interact through digital demonstrations, interactive screens, and displayed application examples. Rather than a conventional exhibition space, it will function as a technical consultation area designed to foster discussion, simulation, and a deeper understanding of manufacturing challenges and solutions. Through this approach, Sandvik Coromant aims to make digital and software-based manufacturing solutions more tangible and accessible, helping visitors explore how integrated technologies can improve performance and process control. A key focus will be CoroPlus® digital machining solutions, which will highlight how data-driven capabilities can support process optimization, improved tool and software integration, and greater control of manufacturing operations. The company will demonstrate how this approach enables manufacturers to improve productivity, operational efficiency, and process predictability. This evolution reflects Sandvik Coromant’s broader transformation from a tool supplier to a technology partner in connected manufacturing, supporting the development of digital and flexible manufacturing environments based on data, performance and process control. Additionally, Sandvik Coromant will participate in the BI-MU FutureTech competition, the official initiative that recognizes innovative solutions presented at the fair. This participation underscores the company's commitment to technological innovation, digitalization, and sustainability, and strengthens its position in the development of next-generation manufacturing. "BI-MU is an important opportunity for us to showcase our ongoing transformation and our focus on digital manufacturing solutions," said Antonio Principe, Sales Cluster Manager at Sandvik Coromant. "Our booth concept reflects our evolution from tool supplier to technology partner, helping customers connect data, processes, and performance." Visitors are invited to visit the Sandvik Coromant stand in Hall 22 to meet with experts and learn how connected and digital manufacturing solutions can support the transition to more efficient, data-driven production systems. Sandvik Coromant Together with our customers and partners, Sandvik Coromant is paving the way for a sustainable future, providing tooling solutions to mechanical industries worldwide. Over eighty years of field experience have allowed us to acquire a wealth of knowledge in the field of metalworking. This expertise transforms every challenge into an opportunity for innovation, collaboration, and cutting-edge solutions. Our goal is to create positive change by promoting sustainability, efficiency, and growth to shape a future where innovation thrives. Part of the global Sandvik industrial group, Sandvik Coromant is shaping the future together. For more information, visit www.sandvik.coromant.com or join the conversation on social media.
 Industriale.it certification